
News
TEL:18925129293


What is a planetary vacuum mixing and defoaming mixer? How does it differ from centrifugal defoaming and blade stirring?
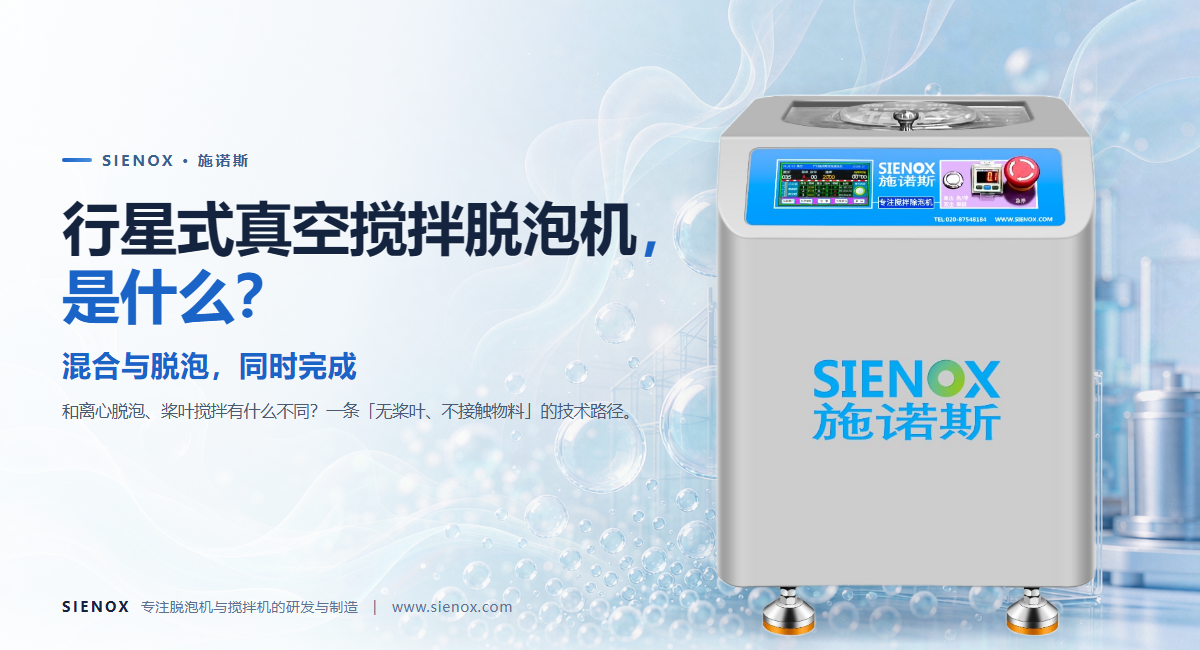
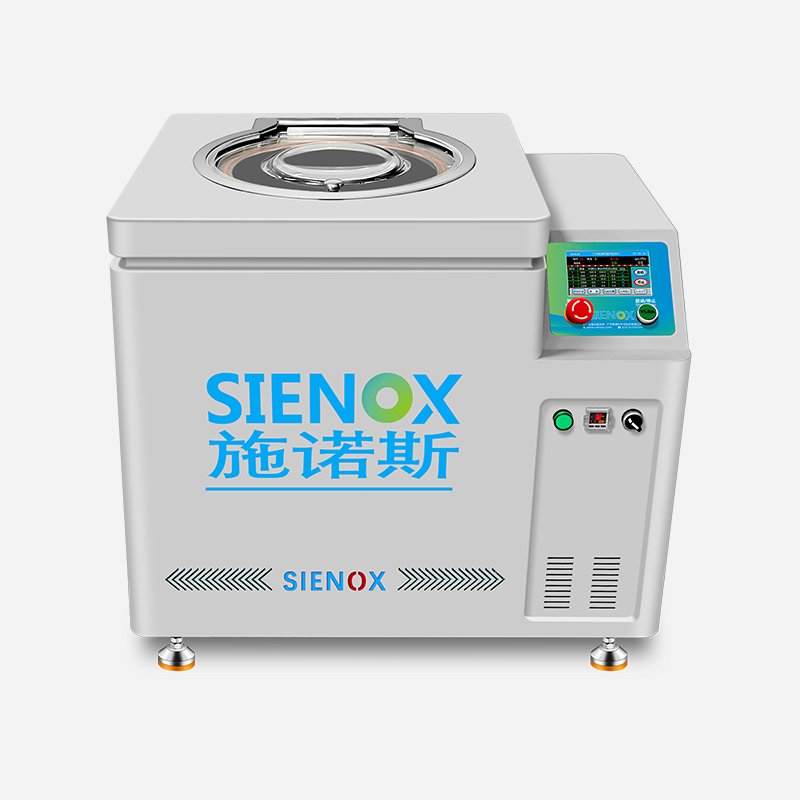
日期:2026-11-03作者:小施SIENOX Planetary Vacuum Mixing & Defoaming Mixer adopts an impeller-free non-contact design. It mixes materials through planetary revolution and rotation movement, and completes mixing and defoaming simultaneously with a vacuum system. The standard vacuum level is -98 kPa. SIE-MIX60 handles 0–300 mL per batch, while SIE-MIX1000plus handles 0–1000 mL per batch. It solves the conflicting problem of high-viscosity materials: uneven mixing and incomplete bubble removal.
1. Definition and Working Principle
The operation of a planetary vacuum mixing and defoaming mixer consists of three synchronized actions:
Revolution: The material cup revolves around the main spindle of the equipment, turning the whole material mass and ensuring uniform force distribution across all zones inside the cup.
Rotation: The material cup spins around its own axis at the same time, disturbing the internal flow field and preventing the material from rotating passively together with the cup.
Vacuuming: The sealed chamber is evacuated to a standard vacuum of -98 kPa (-100 kPa optional). Reduced pressure makes internal bubbles expand, rise and rupture under pressure difference.
Mixing and defoaming are finished in one single cycle. The whole process is impeller-free and non-contact — materials only touch the inner wall of the cup. This is the fundamental difference from traditional blade stirring.
2. Comparison of Three Defoaming Methods
Comparison Item | Blade Stirring (Atmospheric / Vacuum) | Centrifugal Defoaming | Planetary Vacuum Mixing & Defoaming |
Mixing Method | Shearing by immersed blades | Bubbles separated by centrifugal force, limited mixing capacity | Planetary revolution + rotation, non-contact |
Material Contact | Contact | Non-contact | Non-contact (impeller-free, material only touches cup wall) |
Risk of Metal Contamination / Shear Damage | Shear exists; blade wear may introduce foreign particles | No shearing | Impeller-free, no metal contamination risk |
Mixing Dead Zone | Dead zones near blade root and tank wall | No mixing action, risk of material stratification | Material tumbles with planetary motion, no dead zone |
Cleaning | Complex blade structure, risk of residue | Simple structure | No internal blades, no cleaning residue |
Applicable Viscosity | Wide range | More effective for low & medium viscosity | Outstanding for medium & high viscosity (subject to actual test) |
Summary: Blade stirring works by "shearing", centrifugal defoaming by "throwing bubbles out", and planetary vacuum mixing & defoaming completes mixing and defoaming simultaneously via "tumbling + spinning + vacuum evacuation".
3. Typical Process Workflow (Thermal Conductive Potting Compound as Example)
The viscosity and duration data below are typical reference values, subject to on-site test results.
Background: For electronic potting applications, two-component thermal conductive potting compound features high solid content and high viscosity. Manual stirring leaves internal bubbles, which cause shrinkage cavities after curing.
Difficulty: Bubbles rise extremely slowly under high viscosity; static defoaming under atmospheric pressure is impractical. Thermal conductive fillers in potting compound are shear-sensitive; blade stirring may damage filler dispersion and introduce metal contamination from blade wear.
Selection Reason: This scenario requires one-step mixing and defoaming, non-contact impeller-free design and high vacuum capability — exactly the strengths of planetary vacuum mixing and defoaming mixers.
Process Steps:
Load proportioned material into the mixing cup, filling volume within the recommended range (refer to equipment manual).
Secure the cup, check sealing gasket, then start vacuum pump and pull down to target vacuum (standard -98 kPa, adjust vacuum level according to material).
Set revolution and rotation speed, start at low speed and ramp up after observing material tumbling (SIE-MIX60 max 3000 RPM, SIE-MIX1000plus max 2000 RPM, both stepless adjustable).
Run under vacuum + rotation for a holding period (typically 3–10 minutes, determined by viscosity and loading volume).
Release vacuum slowly to atmospheric pressure, take out material and inspect bubble residue. Repeat the cycle if needed.
Comparison: Before treatment — visible bubbles on surface and internal voids in samples; After treatment — smooth surface and no obvious internal bubbles. Final defoaming performance heavily depends on formulation; sample testing is recommended.
4. Key Parameters of Main SIENOX Models
Parameter | SIE-MIX60 (Gear Drive) | SIE-MIX80 (Belt Drive) | SIE-MIX1000plus |
Batch Capacity | 0–300 mL | 0–300 mL | 0–1000 mL |
Rotation Speed | 0–3000 RPM, stepless adjustable | 0–3000 RPM, stepless adjustable | 100–2000 RPM, stepless adjustable |
Vacuum Level | -98 kPa standard, -100 kPa optional | -98 kPa standard, -100 kPa optional | -98 kPa standard, -100 kPa optional |
Transmission Feature | Gear drive, mature structure | Belt drive, lower noise | Dual cup station, for pilot & small production |
Overall Dimension | 510×430×500 mm | 510×430×500 mm | 820×610×760 mm |
Temperature Control | Optional customized module, not standard | Same as left | Optional customized module (heating / cooling available) |
SIE-MIX60 and SIE-MIX80 share identical core parameters within the 300 mL range; the difference lies in transmission. SIE-MIX80 with belt drive is preferred for noise-sensitive laboratories.
5. Common Misconceptions
Misconception 1: Higher vacuum is always better. The standard -98 kPa (-100 kPa optional) is the upper limit of equipment capability. Vacuum should be tuned by material; low-viscosity liquids may foam violently and overflow at extreme vacuum.
Misconception 2: Maximum speed gives highest efficiency. Excessively high speed may cause obvious temperature rise for certain materials. Temperature control is optional, verify process demand before adding this module.
Misconception 3: Batch capacity equals cup volume. Valid working capacity follows the rated batch range (0–300 mL for SIE-MIX60 / SIE-MIX80, 0–1000 mL for SIE-MIX1000plus), with reserved space for foaming.
FAQ: 5 Frequently Asked Questions about Planetary Vacuum Mixing & Defoaming Mixers
Q1: How to choose between planetary vacuum mixer and centrifugal defoamer? Choose planetary type when high mixing performance and high viscosity are required; centrifugal type works for simple bubble removal with low mixing demand. They are not mutually exclusive.
Q2: What vacuum level can SIENOX defoamers reach? SIE-MIX60, SIE-MIX80 and SIE-MIX1000plus offer standard -98 kPa, optional -100 kPa. Process vacuum is adjusted according to material characteristics.
Q3: Will it introduce metal contamination like blade stirring? The planetary design is impeller-free and non-contact. Materials only touch the cup wall, eliminating contamination from blade wear.
Q4: Which model for small-batch multi-formula lab work? 300 mL grade SIE-MIX60 (gear drive) or SIE-MIX80 (belt drive, quieter). Free sample testing from SIENOX is available for verification before purchase.
Q5: Does the defoamer come with temperature control? Temperature control is an optional customized module instead of standard configuration. Sample testing is recommended to confirm actual process demand.
相关推荐

Centrifugal defoaming machine: An efficient tool for both laboratory and factory.
The extensive application fields of planetary defoaming machines.
How to remove bubbles from glue
The application of vacuum stirring defoaming machine in the defoaming process of silver paste materials.
也许您还需要....
行星式真空脱泡搅拌机 SIE-MIX1000plus
实验室行星式搅拌脱泡机 SIE-SV200
SIENOX行星式脱泡搅拌机 SIE-CV300
离心脱泡机 SIE-C006
About SIENOX
广州施诺斯(SIENOX),20年脱泡机设备研发与生产的源头厂家
超过1800种材料脱泡案例
纳米级脱泡,满足不同材料多段搅拌除泡需要,支持定制
资质齐全,荣获多项国家专利,联系我们可免费试样