

Pressure Degassing Autoclave
TEL:18925129293


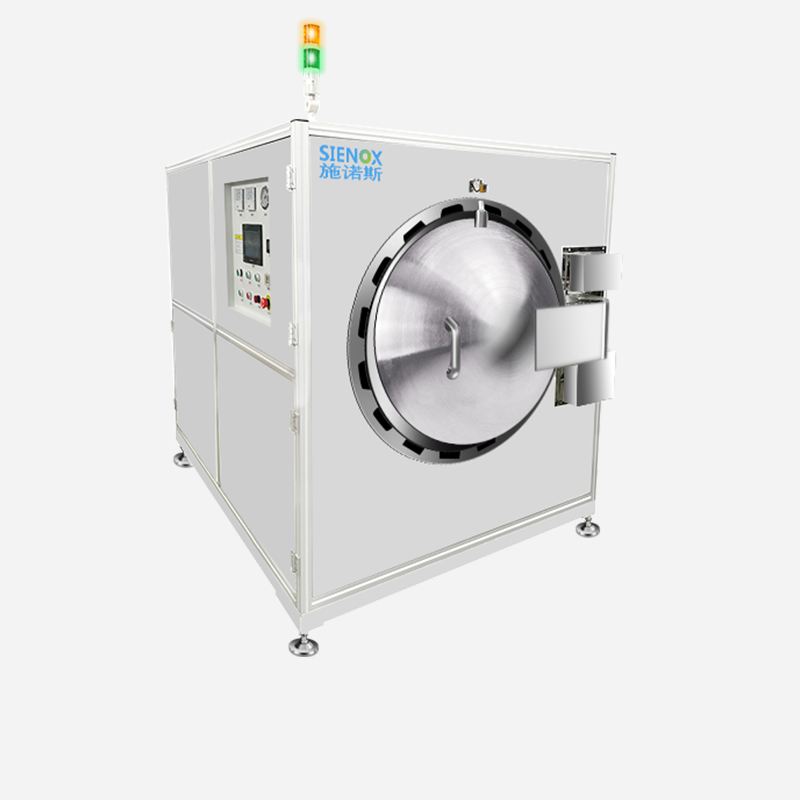
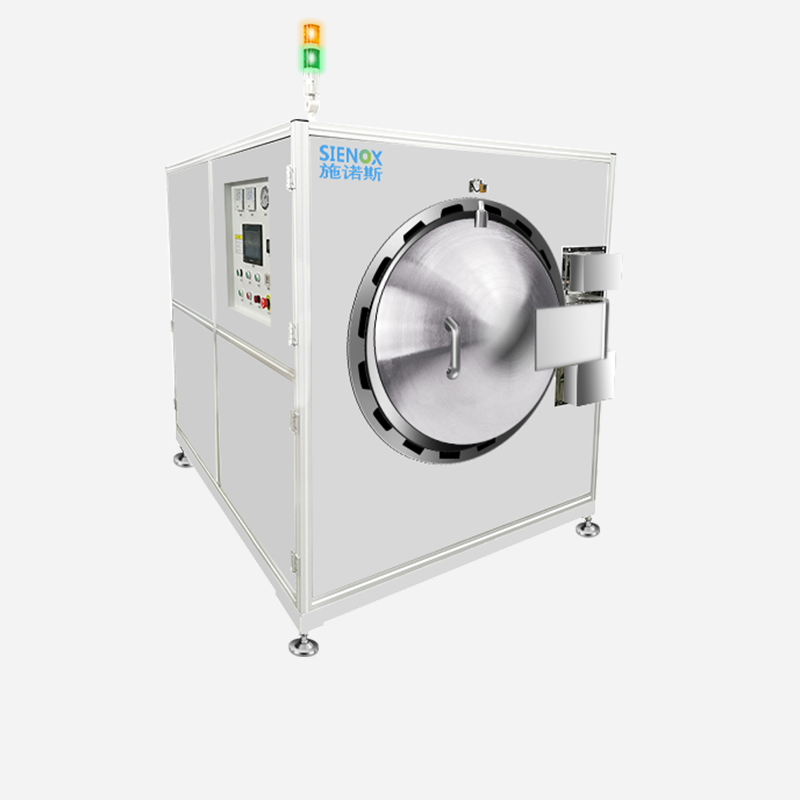
Pressurized Debubbling Machine SIE‑RX10‑1200
Efficient Turnover for Standard‑volume Production · MES Integration for Traceable Process Parameters
Standard‑size Chamber for Efficient Mass Production + MES Linkage for Traceable Process Data + Three‑mode Operation & Audio‑visual‑light Alarm for Safe Operation
SINOS SIE‑RX10‑1200 Pressurized Debubbling Machine is equipped with φ1000×1200 mm cylindrical chamber of approx.940L and supports MES system connection. Three selectable operation modes. SMC digital pressure gauge reaches ±0.01 MPa accuracy, Omron PID temperature control achieves ±1.0 ℃ precision. Pressure rises to 0.6 MPa within 5 min with a single cycle of 35‑40 min. It removes bubbles generated during lamination by temperature and pressure to enhance interfacial bonding strength.
✓ ISO9001 Quality System ✓ RoHS Compliance ✓ Custom‑voltage support (110V/220V)
Why Must Microbubbles in Materials Be Eliminated?
Residual micro‑bubbles degrade end‑product quality directly
Touch Screen Full Lamination IndustryDuring touch‑screen full lamination (G+G/G+F/OCA full lamination), residual bubbles inside OCA optical adhesive reduce light transmittance and cause touch failure. Even a 1% drop in yield will bring huge losses for mass production. The 940 L chamber of pressurized debubbler processes multiple touch screens in one batch. SMC precise pressure control ensures consistent lamination quality for each workpiece. Three operation modes adapt to various OCA adhesives and lamination processes, ideal for standard‑mass debubbling of touch‑screen full lamination. | LED Display Module IndustryBubbles in LED display‑module potting adhesive and drive‑power potting compound lead to dead lamps, dark spots and poor heat dissipation. Stable debubbling is essential to guarantee module quality in mass production. Omron PID temperature control improves the fluidity of potting adhesive for easier bubble removal. The 940 L chamber boosts throughput by processing multiple modules per cycle, and audio‑visual‑light alarm ensures safety for long‑time mass‑production operation. | Electronic Packaging Material IndustryBubbles in electronic packaging materials such as conductive silver paste, insulating adhesive and underfill cause voids in packaging layers and broken conductive paths, requiring stable batch debubbling for volume manufacturing. Microcomputer control stores and reproduces process parameters, and precision filter prevents secondary contamination of packaging materials. The 940 L chamber fits batch debubbling for standard mass production of electronic packaging materials with full traceable process parameters. |
✨ Standard mass production requires connection with production management systems, yet ordinary debubbling devices fail to support MES docking, resulting in untraceable and unmanageable process parameters. Conventional equipment suffers from high failure rates during long‑hour continuous mass operation. Without audio-visual-light alarm systems, operational abnormalities cannot be detected in a timely manner. Insufficient single-batch capacity leads to frequent batch splitting and queuing, disrupting production rhythms and delaying delivery schedules.
Why Choose SIE‑RX10‑1200
Resolve Efficiency, Management and Safety Pain Points for Standard Mass Production
Standard Capacity for High‑efficiency Mass ProductionThe cylindrical chamber reaches approx. 940L with large single‑batch loading capacity. Each full cycle lasts 35‑40 min including 15‑30 min effective debubbling time for high throughput per unit hour. The 940L chamber suits batch loading of standard‑size workpieces such as touch screens, LED modules and packaging materials. Multiple pieces can be processed in one run to match production‑line tact time requirements. | MES‑System Integration SupportCompatible with MES production‑management system for uploading and tracing process parameters, as well as managing and analyzing production data. Parameters including pressure, temperature and duration of each batch are automatically recorded during mass production. Quality issues can be traced to specific batches and parameter records, meeting factory‑audit and quality‑management requirements. | Three‑mode Operation & Audio‑visual‑light AlarmThree operation modes adapt to various lamination processes, enabling one machine to serve multiple production‑line demands. The audio‑visual‑light alarm triggers synchronized notifications upon abnormalities, with alarm messages displayed on microcomputer panel. Failures can be detected and handled promptly even during long‑run mass production to lower the risk of batch scrap. |
✨ If you need MES‑system integration, high throughput and reliable safety assurance for standard mass production, RX10‑1200’s standard chamber capacity and MES connectivity can satisfy your volume‑manufacturing management requirements
Working Principle
Remove bubbles generated during lamination by pressure and temperature to enhance bonding strength between different materials.
Step 1: Pressurization & Heating (3 modes optional): Select pressure first then heating, simultaneous heating & pressurization or heating first then pressure according to material properties. Resistive heating combined with pressurization builds the defoaming environment. Step 2: Pressure Holding & Defoaming: Maintain constant pressure and temperature. Pressure compresses and dissolves bubbles on bonding surfaces; heat reduces material viscosity to help bubbles escape from bonding interfaces. Step 3: Pressure Relief & Stabilization: Slowly release pressure to atmospheric pressure. The adhesion between materials is enhanced, and bubbles on bonding surfaces are eliminated. Three simple steps: Pressurization & Heating → Pressure Holding & Defoaming → Pressure Relief & Stabilization, eliminating bonding bubbles and boosting adhesive strength. | 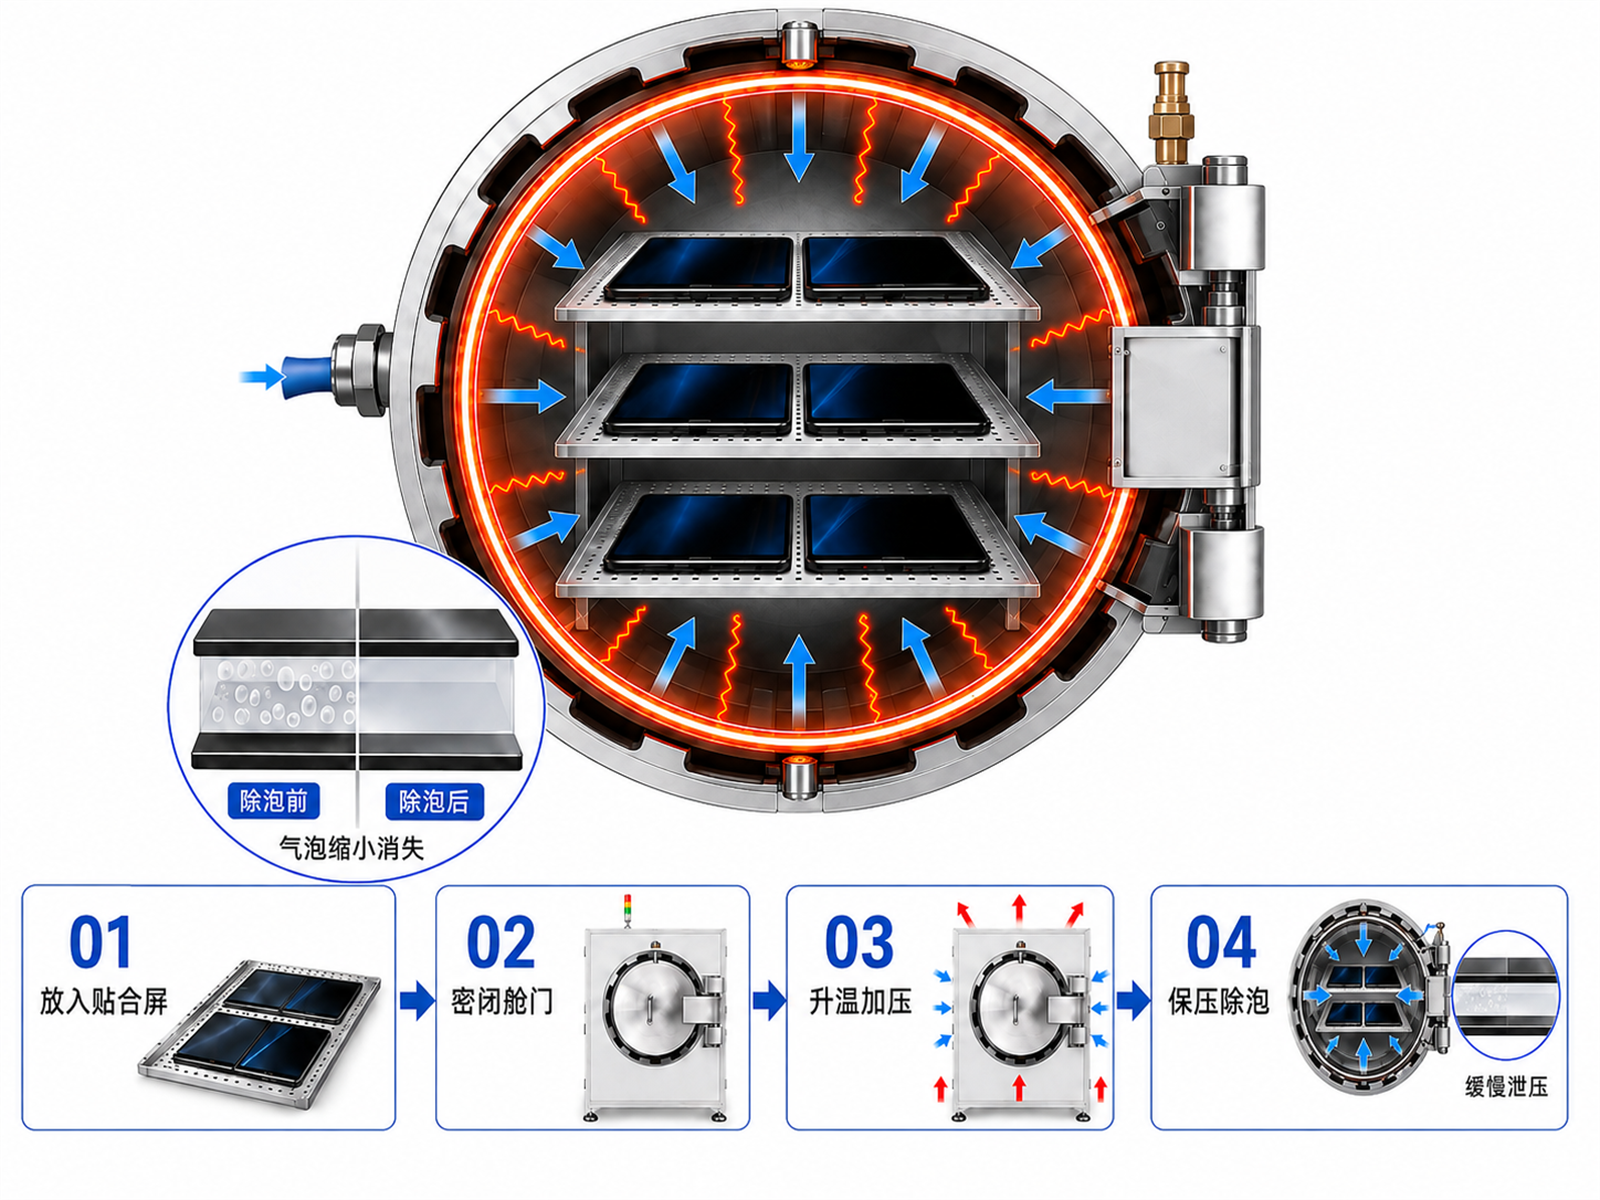 |
Technical Specifications
Complete Technical Specifications Overview, Customizable on Demand
| Model | SIE‑RX10‑1200 |
| Chamber Size | φ1000×1200mm (Cylindrical) |
| Effective Volume | Approx. 940L |
| Working Pressure | 0~0.8MPa (Standard), 0~2.5MPa (Optional) |
| Working Temperature | Ambient ~80℃ (Standard), Ambient ~180℃ (Optional) |
| Heating Method | Resistive Heating |
| Operation Modes | A. Pressurize First Then Heat B. Simultaneous Heating & Pressurization C. Heat First Then Pressurize |
| Control Mode | Microcomputer Control |
| Vessel Material | S30408 Stainless Steel or Carbon Steel |
| Overall Dimension(W×D×H) | Approx. 1300×1500×2000mm (Subject to actual product) |
| Net Weight | 1500 kg |
| Certifications | ISO9001, RoHS Compliance |
我们的合作伙伴
深受全球知名工业制造集群及前沿高校实验室信赖
FAQ 您关心的问题
为您解答关于产品性能及日常工艺选型中的常见疑问
-
真空脱泡搅拌机是什么?用于哪些行业?
真空脱泡搅拌机是在真空环境下同步完成搅拌与脱泡的设备,脱泡同时混料,避免二次气泡混入,常用于环氧树脂、硅胶、AB 胶等高粘度材料的混料脱泡处理,广泛应用于新能源电池、半导体封装、LED、电子灌封、胶粘剂等行业。
-
广州施诺斯主要生产哪些设备?
主要产品包括搅拌脱泡机、真空脱泡搅拌机、真空脱泡机、高压脱泡机、真空搅拌机、实验室均质机、三辊研磨机、三维混粉机,以及点胶机、分装机等配套设备和夹具、搅拌罐、针筒等辅品耗材。
-
源头厂家采购脱泡设备有什么优势?
源头厂家直供可省去中间环节,价格更透明,同时能提供参数定制、来料试机、工艺验证等服务,售后响应更直接。
-
搅拌脱泡机的工作原理?
施诺斯设备采用行星式混合原理:料罐在自转的同时绕公转轴公转,物料在罐内随之翻动混合,同时抽真空脱泡。整个过程设备不设搅拌桨,搅拌部件不接触物料,不会引入金属异物,混合均匀不分层。
-
为什么选择施诺斯?
施诺斯(SIENOX)是广州施诺斯科技股份有限公司旗下品牌,2014 年成立,专注脱泡机与搅拌机的研发与制造,团队自 2006 年起从事真空搅拌脱泡设备研发。设备采用非接触式设计,不设搅拌桨,行星式公转加自转运动辅以真空系统,高效除泡,混合均匀不分层。公司产品涵盖搅拌脱泡机、真空脱泡搅拌机、真空脱泡机、高压脱泡机、真空搅拌机、实验室均质机、三辊研磨机、三维混粉机,以及点胶机、分装机等配套设备和夹具、搅拌罐、针筒等辅品耗材,广泛应用于新能源、半导体、LED、电子灌封、胶粘剂、涂料、油墨等行业。通过 ISO9001、CE 认证,拥有 30 余项专利,服务富士康、比亚迪、清华大学等企业与科研院所。
Multi‑Model Specification Comparison Table
Compare Models in the Same Series for Accurate Selection
| Model | SIE‑RX6‑900 | SIE‑RX8‑1200 | SIE‑RX10‑1200 |
| Chamber Size | φ600×900mm | φ800×1200mm | φ1000×1200mm |
| Effective Volume | 255L | 600L | 940L |
| Pressure Range | 0~2.5MPa(Optional) | 0~2.5MPa(Optional) | 0~2.5MPa(Optional) |
| Temperature Range | Ambient ~180℃(Optional) | Ambient ~180℃(Optional) | Ambient ~180℃(Optional) |
| Pressure Accuracy | ±0.01MPa | ±0.01MPa | ±0.01MPa |
| Temperature Control Accuracy | ±1.0℃ | ±1.0℃ | ±1.0℃ |
| Power Supply | 220V, 50/60Hz (Customizable for 110V US/JP standard) | 220V, 50/60Hz (Customizable for 110V US/JP standard) | 220V, 50/60Hz (Customizable for 110V US/JP standard) |
| Overall Dimension(W×D×H) | 610 × 560 × 780 mm | 610 × 560 × 780 mm | 1300×1500×2000mm |
| Net Weight | 153 kg | 163 kg | 1500 kg |
***Above are typical models. Customized solutions are available upon customer requirements.
Multi‑Industry Solutions
Covering stirring and debubbling applications of typical materials across six major industries
LCD Polarizer LaminationSmall‑size polarizer OCA optical adhesive, lamination adhesive for LCD glass substrate |
Electronic Component EncapsulationComponent encapsulant, chip potting adhesive |
Medical DevicesMedical bonding adhesive, medical‑device lamination adhesive |
LED EncapsulationLED encapsulant, phosphor paste |
Fine ChemicalsFine chemical materials, nano‑powders |
New Energy MaterialsR&D samples of new energy materials, battery paste samples |
Comprehensive Equipment Operation Demo Videos
Gain intuitive, clear, dynamic insight into synchronous defoaming with planetary centrifugal force and high negative pressure.
:Actual‑test Performance Demonstration
Measured Processing Results for Six Typical Materials
Slurry + Powder |
Adhesive |
Hydrogen Energy Materials |
Adhesive |
Substrate + Filler |
Adhesive + Ceramic Powder |
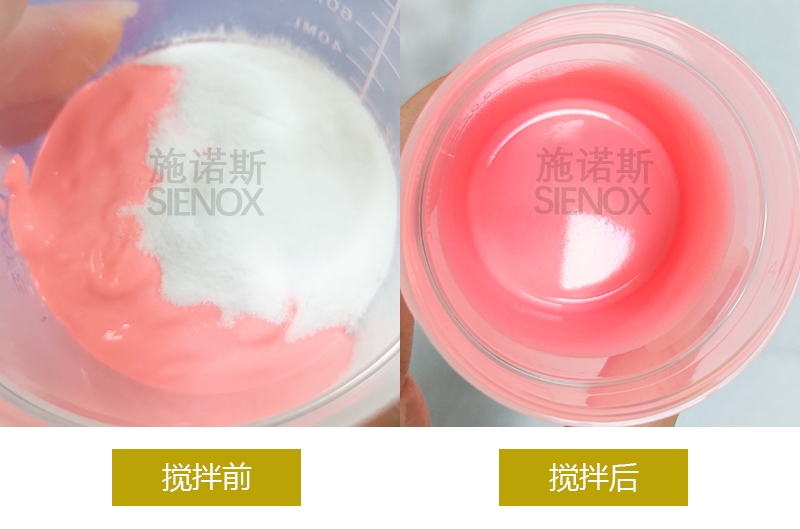
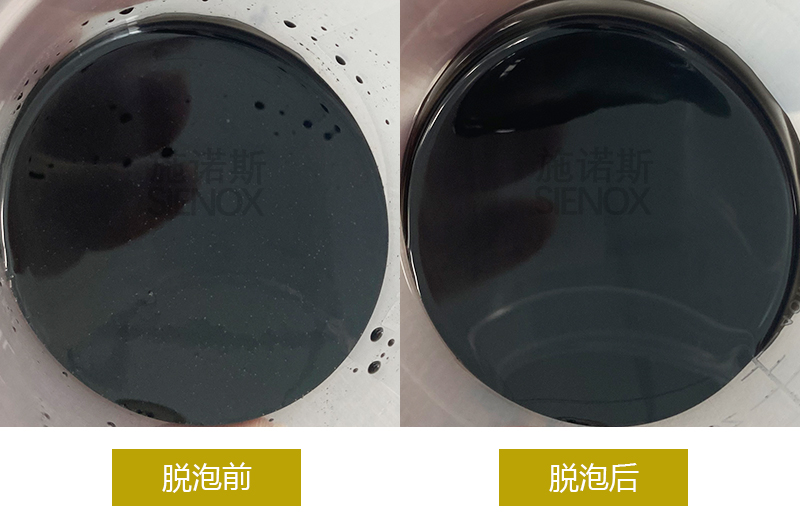
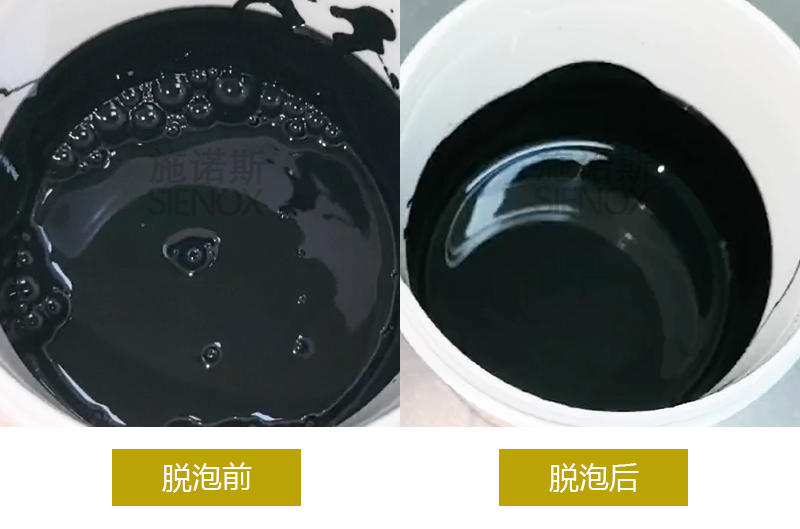
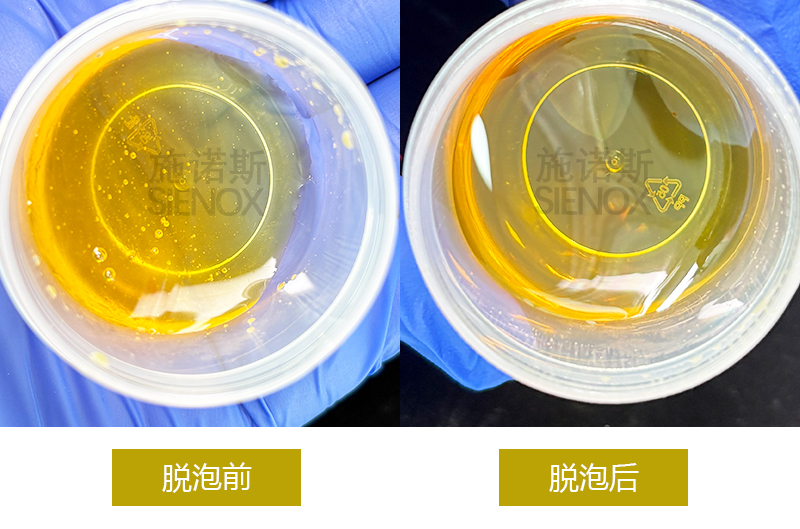
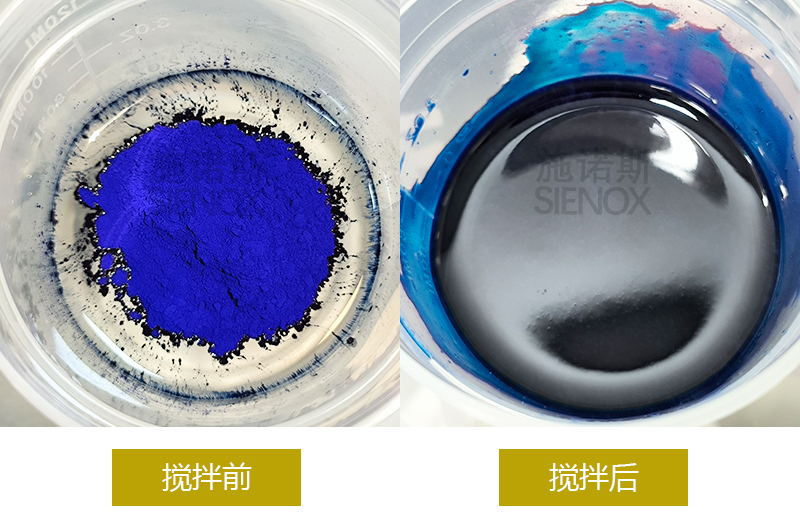
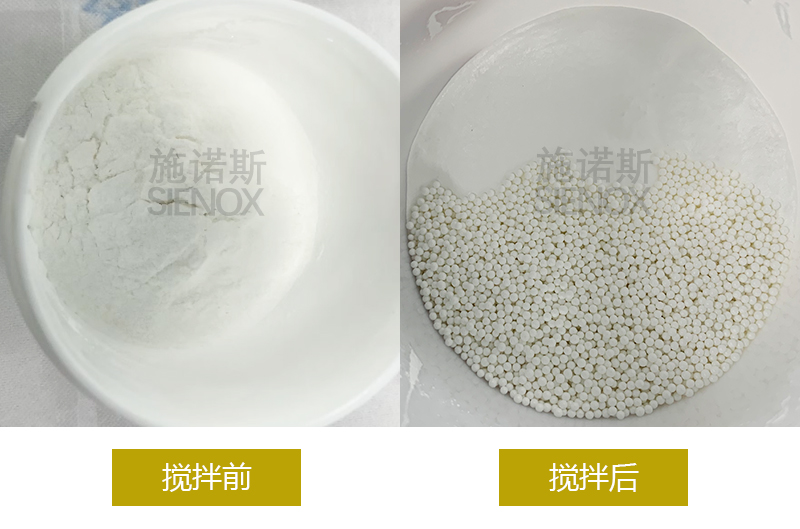
Actual‑test Effect Comparison
Comparison of Material Status Before and After Pressurized Debubbling
| Material Type | Pre‑treatment Status | After SIE‑RX10‑1200 Treatment |
| Polarizer OCA Optical Adhesive | Numerous internal bubbles, uneven light transmission & mottling after lamination | Bubble‑free transparent adhesive with uniform light transmission after lamination |
| Component Encapsulant | Dense inner bubbles, voids formed in encapsulation layer after curing | Dense void‑free adhesive for complete and reliable encapsulation layer |
| Medical Bonding Adhesive | Internal bubbles cause bonding‑surface defects and impair biocompatibility | Dense adhesive with intact bonding surface and qualified biocompatibility |
* Internal laboratory test data. Actual improvement varies with material formulation. Contact sales for real‑world customer cases.
Customer Delivery & Application Cases
Rooted in manufacturing frontlines, empowering benchmark production lines and key national research institutions across diverse industries.